
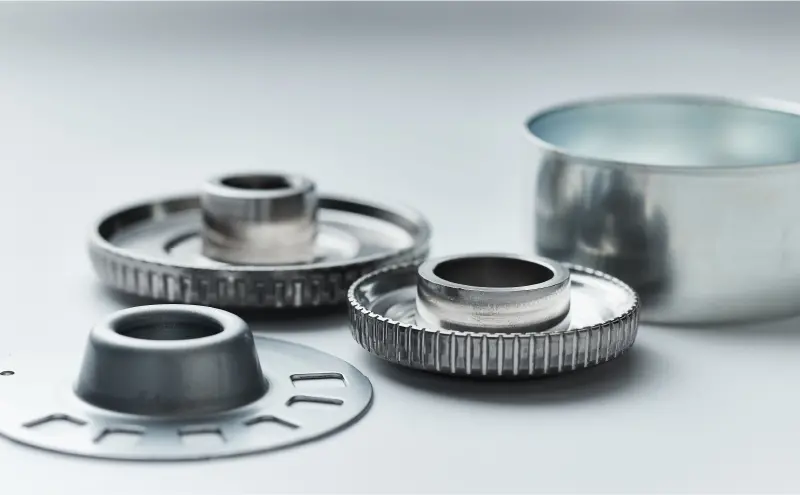
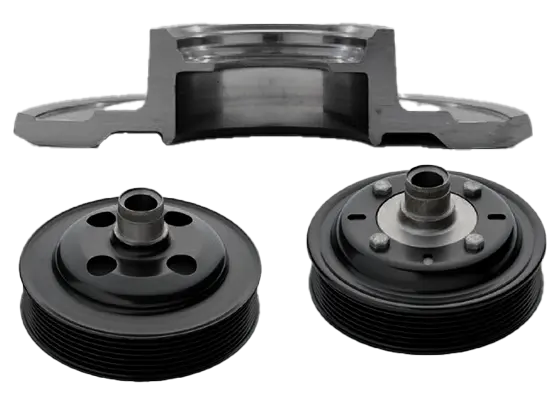

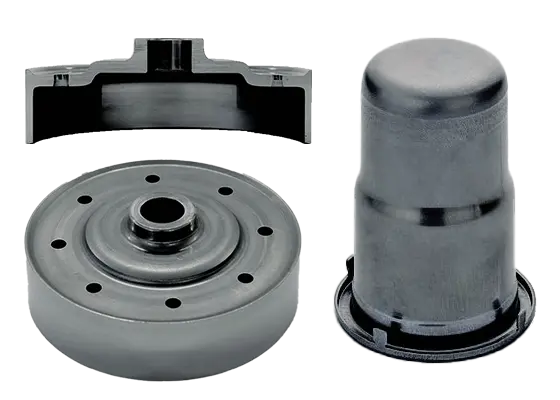


The process design carefully considers the metal flow and an effort is made to increase the product strength. Also, thickening technology is used to add thickness at the points where it is required so that it is possible to increase the strength and also superior quality stability is achieved
Locally changed thickness High hardness
It is possible to reduce the weight of the product by thickening or thinning the material in particular areas.
Weld-free Integration
It is possible to realize a boss and a circular steel plate as a single part by using the “Integrated Boss Forming Method” to form a thicker par t (boss) in the center of a circular steel plate. This means that no joining by welding or bolt tightening is required and also it is possible to form a keyway or spline on the boss at the same time.
Cut-free Manhour reduction
This is original technology to form three dimensional shapes
from steel plate. Cup-shaped semi-finished products are
rotated and the shape required is formed using a roller
Thickening to about three times material thickness is possible (periphery)
It is possible to increase or decrease the thickness of certain parts and strain hardening means that the parts made thicker/thinner are harder than on cast items, so the functions required can be satisfied with products with thinner profiles and also weight reduction is possible.
The “Roll-Forming Technique” does not apply heat and there are no metal chips produced, so it makes maximum use of the raw materials and realizes a high material yield. Also, the elimination of a cutting process means that processing times are greatly.
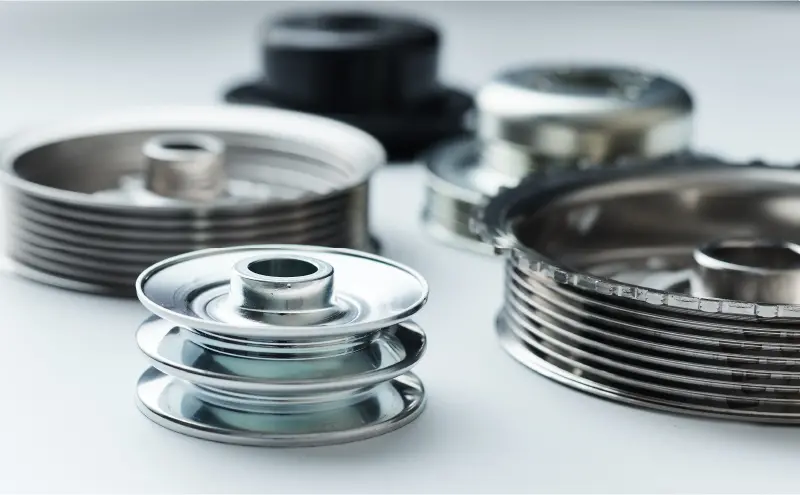
The product is rotated as it is formed, so this greatly improves the surface roughness on the product and creates a lustrous glossy surface.
The “Roll-Forming Technique” does not apply heat and there are no metal chips produced, so it makes maximum use of the raw materials and realizes a high material yield.
Merits
● It is possible to use the internal mold and external roller to work from both sides to form the uneven shapes required in the material.
It is possible to increase the inner and outer diameters of ring-shaped product materials with forming rolls.
Merits
● The pipe material can be expanded to twice the size of the material in the radial direction. It is possible to form pipe-shaped materials at sizes not available on the market.
● Increased hardness due to strain hardening.
● Even high hardness materials can be processed.
Expansion
About twice the material’s diameter
φ100㎜→φ180㎜
The inner diameter of products can be thinned with a small roller as the deep drawing is performed.
Merits
● It is possible to create designs with a high degree of freedom with some parts that are extremely thin, so it is possible to
reduce weights and material costs.
● It is not necessary to perform the annealing process that is necessary for deep drawing using press working.
● Extra-deep drawing using a compact roller dramatically improves surface roughness. A beautiful gloss is created.
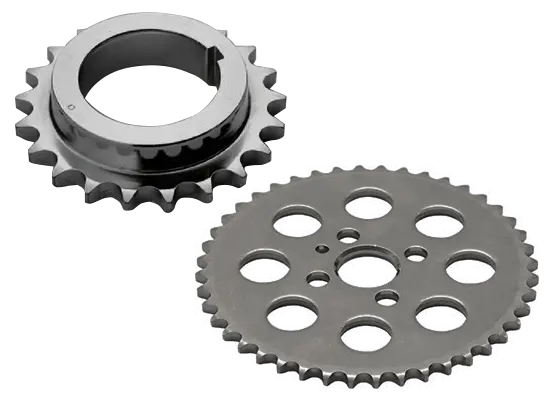
The Kanemitsu “Precision Press Cutting Method” realizes precision
tooth thickness of 6 mm and above and 90% shear plane on the
part punched out without using dedicated special equipment or
special molds. Products formed using the “Precision Press Cutting
Method” have the excellent merits that they have higher
toughness and abrasion resistance than products processed with
sintering and cutting.

Kanemitsu has continued to realize “Unique Manufacturing” by considering the issues together with the customer and always acting as a technology partner that can be relied on for “Manufacturing” using steel plates.
We are currently working to steadily prepare development and production systems so that we can use the technology we have developed as a top manufacturer of automobile engine pulleys and apply and extend it to products in various other sectors.

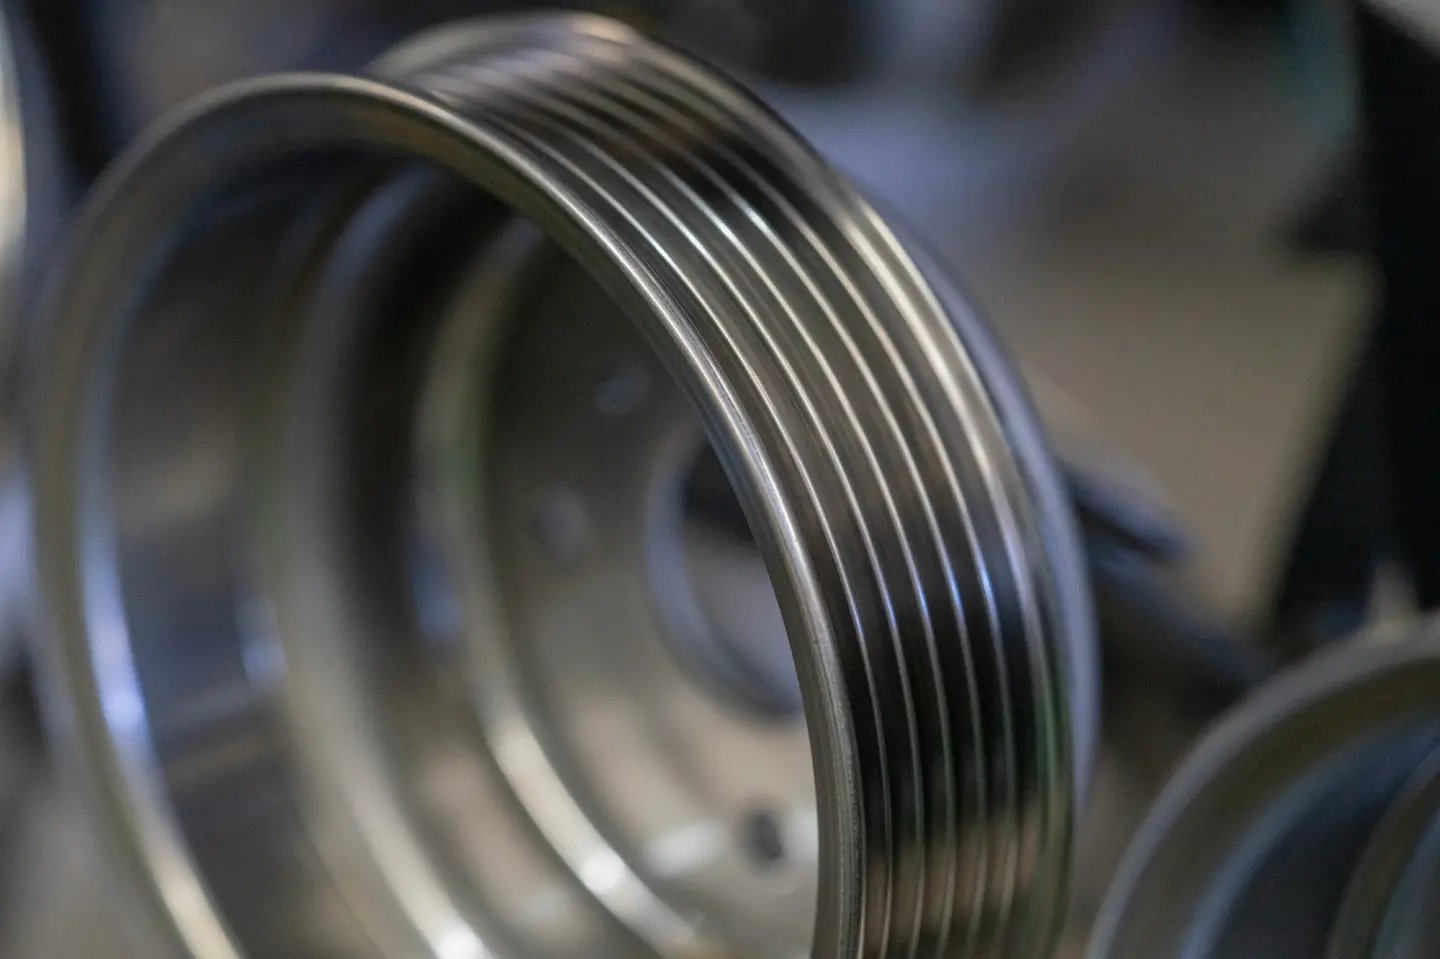
In addition to the profiles and precision, we are also pursuing the development of techniques that utilize the characteristics of the materials such as the metal structure and we are conducting research and development that also considers the product functions and the later processes to be performed by the customer. We are also working to reduce the total cost through equipment development and automation to fit those processes. In addition, we conduct company-wide “Concurrent Engineering” from the initial stages and respond to the customer requirements rapidly and carefully.
Kanemitsu has original technological expertise and develops all the molds and “Roll-Forming Equipment” in-house to realize improved product precision and cost reductions. We achieve more precise operations with CAE systems that make it possible to conduct advance verification from the design phase.
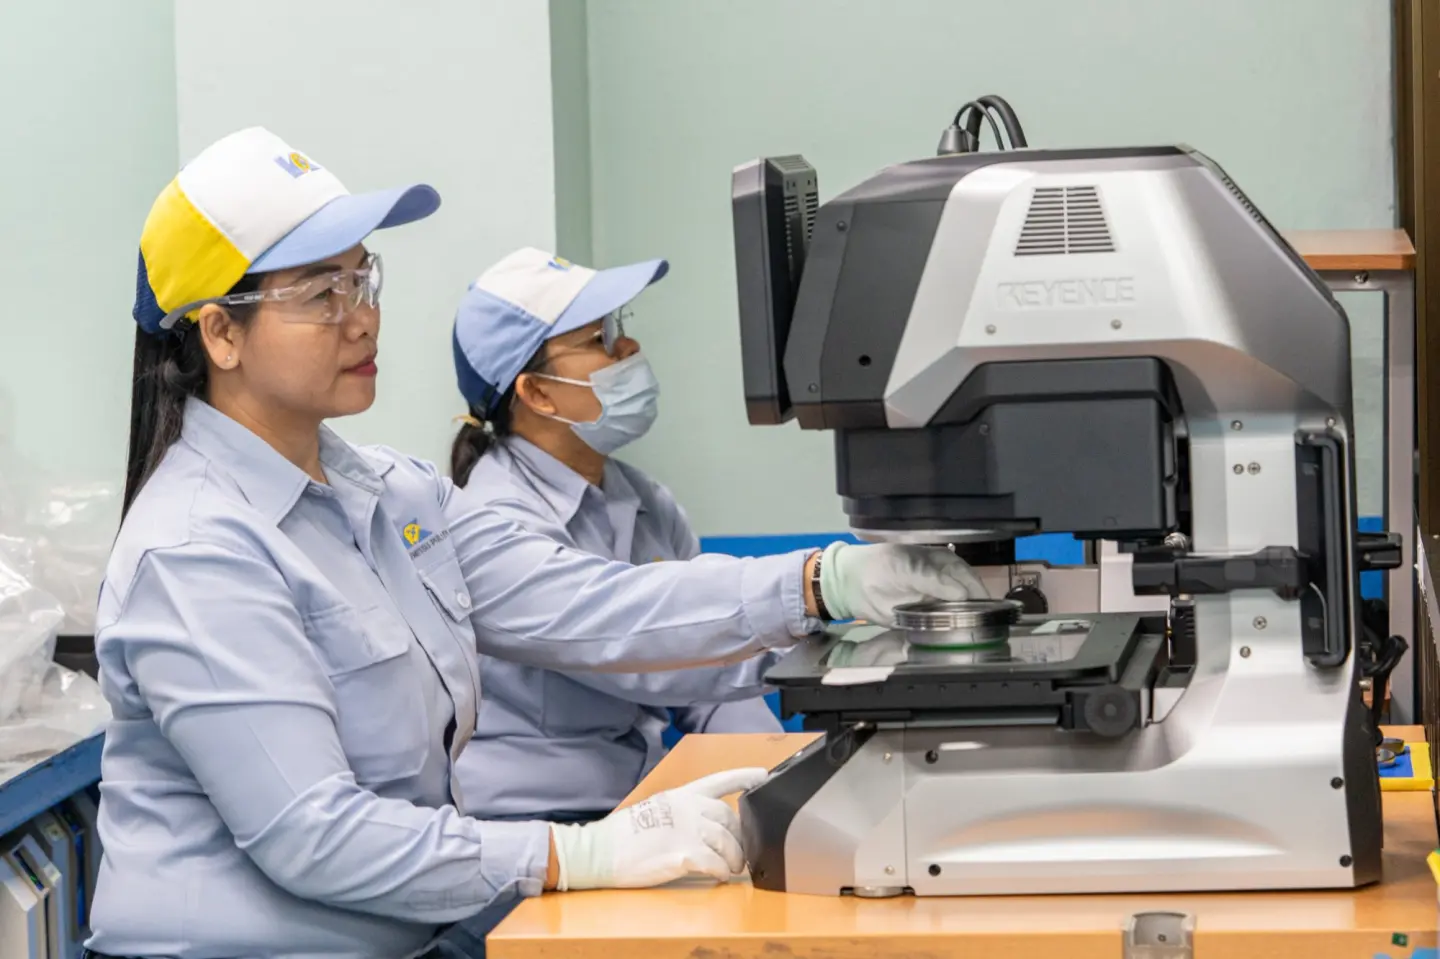
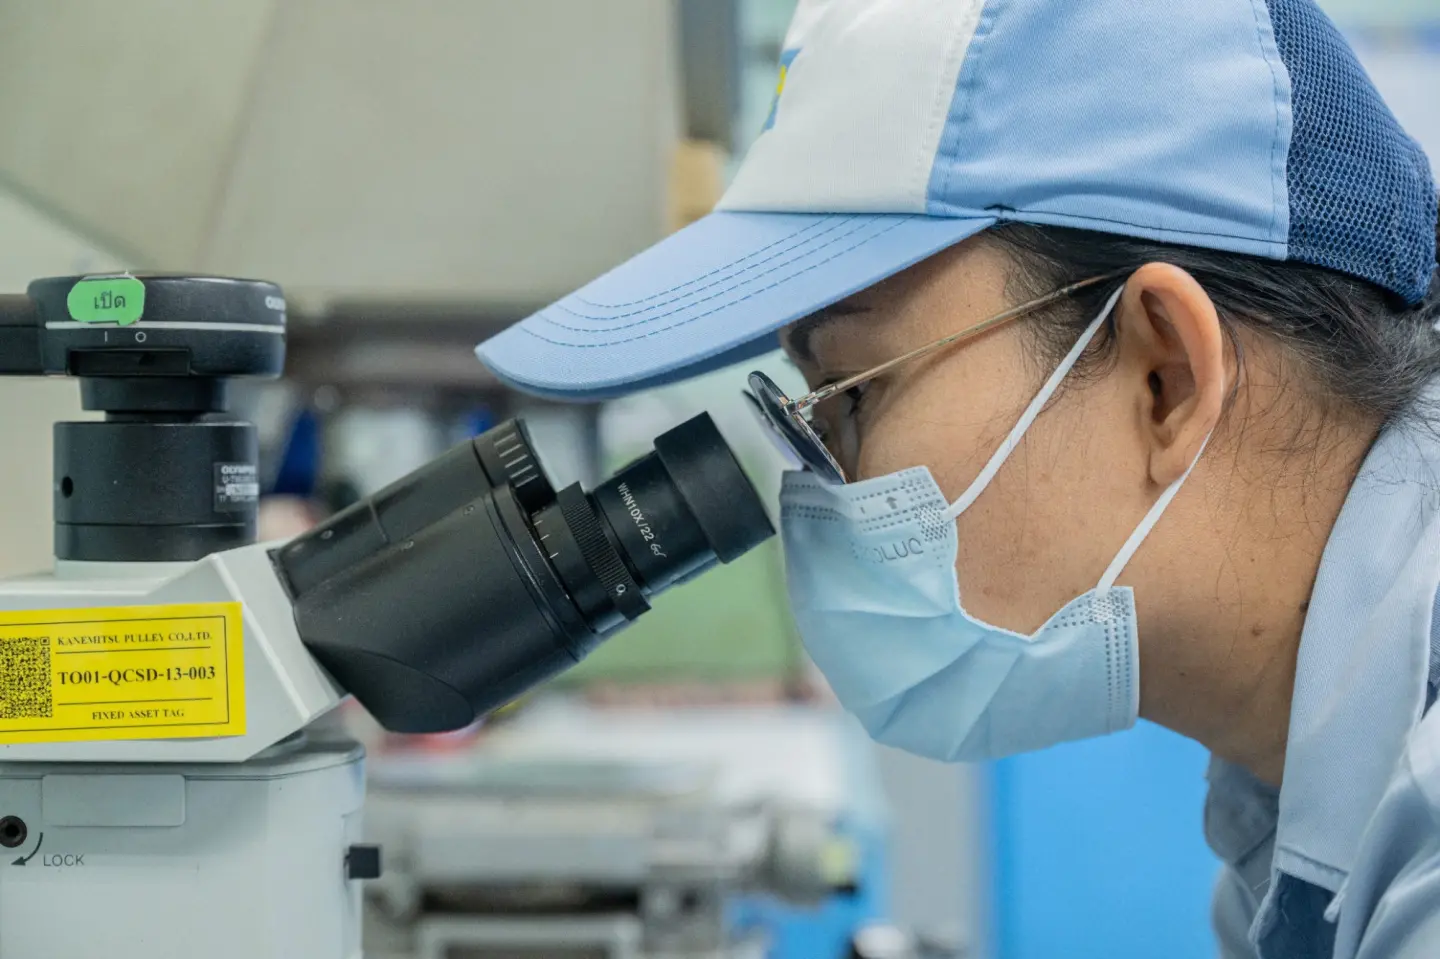
We build in quality by conducting thorough reviews and using trial production equipment based on the mass production equipment.
We are also preparing a system for the quick and high-precision evaluation of the product functions required by the customer, such as our original “Bench Test Equipment for Product Strength Guarantees” (developed in-house) and “3D Coordinate Measuring Machines.”